Choosing a Medium-Sized Wave Soldering Machine requires more than comparing conveyor width and price. The right choice must fit your boards, solder volume, flux chemistry, and production rhythm. A machine that handles one 400-millimeter assembly may struggle with another. Thermal mass changes everything.
Ray Prasad, a recognized author and specialist in surface-mount and wave-soldering processes, offers a useful principle: “Choose equipment by process capability, not by footprint alone.” This idea guides the outline ahead. It examines conveyor stability, preheat zones, solder-pot design, nozzle access, nitrogen options, and control software. It also considers practical details, such as whether operators can clean the pot safely and reach filters without dismantling half the machine.
Experience on a factory floor often exposes weaknesses that brochures hide. A compact machine may consume less space, yet require frequent adjustments. A larger model may provide steadier temperature control, but waste energy during low-volume production. These trade-offs deserve honest testing.
The selection process should begin with real assemblies, not ideal samples. Record board dimensions, component clearances, solder alloy, line speed, and defect patterns. Ask suppliers for process data and a production trial. Independent verification remains valuable.
There is no universal best machine. That sounds obvious, but it is often ignored.
A reliable Medium-Sized Wave Soldering Machine should deliver repeatable joints, manageable maintenance, operator safety, and measurable support after installation. This introduction will help readers compare those factors carefully, while recognizing one uncomfortable truth: specifications alone cannot prove production success.
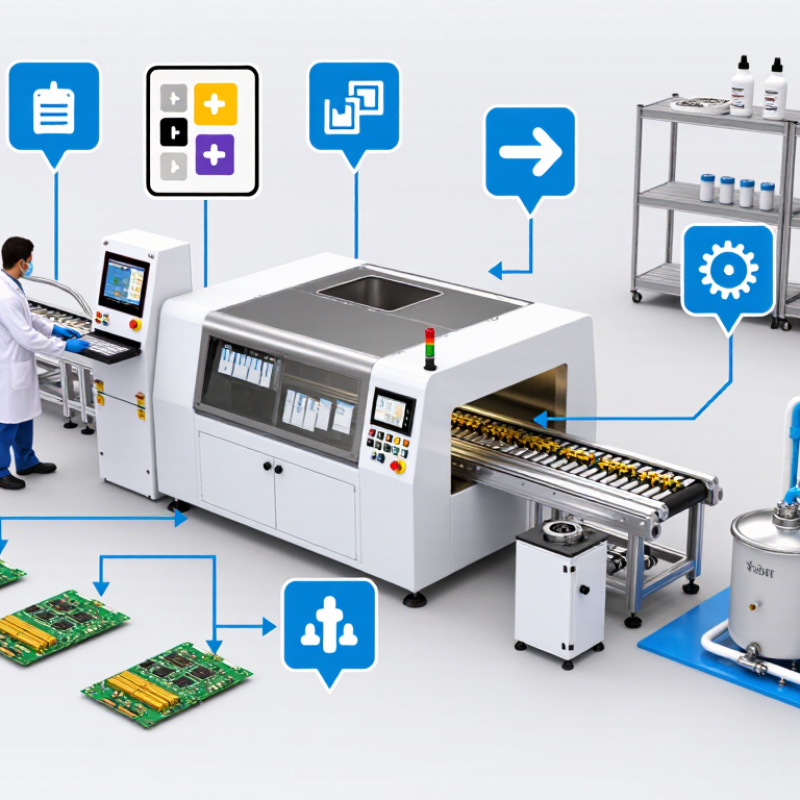
Before choosing a medium-sized wave soldering machine, define the line’s actual workload. Record boards per hour, shift length, changeover frequency, and likely peak demand. Average output can hide bottlenecks when urgent orders arrive. Peaks matter. Allow time for loading, inspection, and routine pauses; theoretical conveyor capacity rarely matches a full shift. One early estimate may still be too optimistic, so compare it with production records.
Measure the smallest and largest boards, including thickness, width, and conveyor-edge clearance. Note bottom-side components, tall parts, connector locations, and areas that must avoid solder contact. Small details count. Check whether the conveyor can hold each board securely and whether the solder pot, flux application, and preheat zones suit the range of assemblies. Ask process engineers to review representative boards, not just a dimension sheet. Measure twice. A sample run can reveal problems that drawings miss, such as uneven heating or difficult changeovers. Record those findings before fixing machine capacity and configuration.
Define production needs and board specifications before comparing machine capacity.
Illustrative single-lane estimates assume continuous flow and one board per pitch. Capacity is calculated as conveyor speed × 60 ÷ (board length in the travel direction + inter-board gap). For example, a 250 mm board with a 50 mm gap at 1.0 m/min yields about 200 boards per hour. Actual output is lower when stoppages, changeovers, or process limits are included. Also confirm the machine’s usable conveyor width accommodates the board width and required edge clearance.
Conveyor fit
When choosing a medium-sized wave soldering machine, match the conveyor to the boards you actually run, not just your largest product. Check the usable conveyor width, rail adjustment range, and support for different board lengths. Include carriers or pallets in your measurements. A board that fits the rails may still need extra side clearance for components and fixtures. Measure a few representative assemblies before comparing machines.
Production capacity
Soldering capacity must support your target output without forcing rushed settings. Estimate boards per hour, then account for conveyor speed, preheat time, and the contact time needed at the solder wave. Ask how quickly the solder pot recovers after loading and whether temperature stays stable during continuous production. These details affect joint consistency. Capacity figures can be optimistic, so request a trial using your board and process settings where possible. I would not size the machine from peak throughput alone.
Tips: Leave room for expected product changes, but avoid paying for width you will rarely use. Confirm that operators can load boards safely and reach routine service points. Record your board dimensions, carrier needs, and hourly target before requesting a quotation.
For a medium-sized wave soldering machine, compare the heating, fluxing, and solder pot systems as one process. Heating zones should bring boards to a steady temperature without scorching components or leaving cool areas. Ask for temperature readings across a representative board, not just an empty conveyor. Preheat control matters. A specification sheet may not reveal how the machine responds when board thickness or production speed changes.
Tips: Check flux coverage on test boards. Confirm spray consistency across the conveyor width, and ask how easily operators can clean the flux nozzles. Keep records. Small details matter.
The solder pot should hold a stable temperature and support the required wave width and production volume. Check how the machine controls wave height and handles oxidation; these affect solder joints and routine maintenance. Review alloy capacity, access for cleaning, and whether the conveyor accommodates your largest boards. Then run sample assemblies at realistic speeds and inspect joints, not only display readings. Trade-offs are normal: a compact machine may save floor space, but leave less room for wider boards or future capacity. Recheck the chosen settings after a full production shift.
A medium sized wave soldering machine should have controls that make temperature, conveyor speed, and flux settings easy to check. A clear display helps operators spot drift before it affects a batch. Keep it readable. Ask for a live demonstration using a sample board, not just a menu tour.
Can operators save approved process settings and review alarm history? These details support consistent production and make troubleshooting less dependent on memory.
Safety features deserve the same close inspection. Check for accessible emergency stops, guarded hot zones, and clear warnings near the solder pot. Confirm that fume extraction can be connected and that its operating status is visible to staff. Small details matter.
Maintenance access also shapes daily reliability: look at how easily technicians can inspect the pump, clean flux residue, and reach filters without awkward tools. Ask how often routine checks are needed and what records should be kept.
Hot components can remain hazardous after shutdown, so procedures must address cooling and isolation. A control panel may look simple in a showroom, yet feel confusing during a shift change; operator feedback is worth gathering before purchase.
How to Choose a Medium Sized Wave Soldering Machine?
Verify Machine Compatibility, Support, and Total Cost of Ownership
A medium sized wave soldering machine should fit your actual production line, not just its rated capacity. Check maximum board width, conveyor height, clearance, and available floor space. Confirm that the machine can handle your heaviest assemblies and required throughput. Ask for a trial using representative boards and your normal soldering materials. Review the thermal profile, solder pot capacity, and exhaust connection. Small mismatches can cause delays after installation.
Tips: Measure the line twice. Request a written installation checklist. Confirm spare-part availability, operator training, and expected response times for service. These details matter when production stops.
Compare the full cost over several years, not only the purchase price. Include energy use, routine maintenance, consumables, training, installation, and likely downtime. Ask suppliers to explain service intervals and which parts typically need replacement. A lower initial quote may hide recurring costs. Still, a spreadsheet can miss the cost of a difficult changeover or limited support. That is worth questioning. Before choosing, compare documented specifications, service commitments, and operating estimates side by side. Keep the assumptions visible, especially projected production hours and maintenance needs.
| Evaluation Area | What to Verify | Practical Evaluation | Impact on Ownership Cost |
|---|---|---|---|
| PCB and pallet compatibility | Confirm the machine’s minimum and maximum PCB width, conveyor adjustment range, board thickness limits, edge clearance, and clearance for tall components. Check pallet dimensions if pallets are used. | Run representative narrow and wide boards, including the heaviest or most complex pallet. Verify stable transport without board interference or component contact. | A mismatch can require custom pallets, line changes, restricted product routing, or a different machine configuration. |
| Soldering process capability | Check compatibility with the required solder alloy, flux application method, preheat zones, wave configuration, and product thermal limits. | Process sample boards using the intended alloy and flux. Assess solder-joint results against the product’s acceptance criteria and applicable workmanship requirements. | Process instability can increase rework, scrap, flux use, solder consumption, and engineering time. |
| Required throughput | Establish the required good boards per hour using actual board dimensions, board spacing, conveyor speed, and solder-contact requirements. Do not rely on conveyor speed alone. | Conduct a timed production trial with representative products and normal operating steps. Record good output, changeover time, and interruptions. | Insufficient net capacity may require overtime, additional shifts, or another production resource. |
| Facility utilities and extraction | Verify the machine’s specified voltage, phase, frequency, connected load, compressed-air requirements, exhaust connection, and heat or ventilation needs. | Compare the machine data sheet with a site utility survey. Confirm exhaust ducting and fume extraction arrangements with the facility team. | New electrical circuits, ductwork, air supply, or ventilation can add installation and operating costs. |
| Footprint and line integration | Check machine length and width, service-access clearances, conveyor height, conveyor direction, and interfaces with upstream and downstream equipment. | Review a scaled layout and confirm maintenance access, material flow, and safe operator access before ordering. | Layout changes can add construction, conveyor, handling, and production-disruption costs. |
| Supplier support and training | Clarify warranty coverage, service response arrangements, installation and operator training, remote troubleshooting, documentation, and local technician availability. | Ask for written service terms, escalation contacts, training scope, and examples of the support process for common faults. | Slow support can extend downtime; training and accessible documentation can reduce setup errors and dependence on external service. |
| Spare parts and maintenance | Request a recommended spare-parts list, expected lead times, maintenance tasks, and replacement intervals for wear items such as filters, nozzles, and conveyor components. | Identify critical parts to keep on site and confirm that maintenance tasks can be completed safely by available staff. | Parts availability and planned maintenance affect repair costs, inventory needs, labor, and unplanned downtime. |
| Total cost of ownership | Compare purchase price, installation, training, utilities, solder and flux consumption, labor, maintenance, spare parts, downtime, and expected resale value. | Use the same evaluation period, operating schedule, production assumptions, and currency for every option. Request written quotations for major cost items. | A lower purchase price may not mean a lower lifecycle cost if installation, consumables, service, or downtime costs are higher. |
| Safety and applicable requirements | Review guarding, emergency stops, hot-surface protection, fume extraction, electrical documentation, and conformity requirements applicable in the installation region. | Have the site’s safety and compliance personnel review the proposed configuration and installation documentation before acceptance. | Unaddressed safety or compliance needs may lead to retrofit costs, delays, or operating restrictions. |
| Planning note: “Medium sized” is not a standardized machine category. Specifications, utility needs, throughput, and operating costs vary by configuration and product mix. Confirm all limits and costs against the supplier’s written specifications and a production trial using representative boards. | |||
Measure usable width, rail adjustment, board length, and carrier size. Leave side clearance for components and fixtures. Measure real assemblies.
Estimate boards per hour, including conveyor speed, preheat time, and solder-wave contact time. Ask about pot recovery and temperature stability. Peak figures can mislead.
Check temperatures across a representative board, not an empty conveyor. Test different board thicknesses and production speeds. Cool spots matter.
Run test boards and inspect coverage across the conveyor width. Ask whether spray stays consistent and nozzles are easy to clean. Keep records.
Check temperature stability, wave width and height control, alloy capacity, oxidation handling, and cleaning access. Inspect joints after realistic trial runs.
It may save floor space but limit wider boards or future output. Choose capacity you expect to use. I might still overestimate future needs.
Demonstrate temperature, conveyor speed, and flux settings with a sample board. Check readable displays, saved settings, and alarm history. A menu tour is not enough.
Check emergency stops, guarded hot zones, warnings, and visible fume-extraction status. Confirm access to pumps, filters, and flux residue. Hot parts remain dangerous after shutdown.
Choosing a Medium-Sized Wave Soldering Machine starts with understanding your production volume, board dimensions, component layout, and soldering requirements. These details help determine the right conveyor width and speed, as well as the machine’s overall throughput capacity. Consider how the heating zones, flux application system, and solder pot can support consistent results across the types of assemblies you produce. Each system should be suitable for your materials, process needs, and expected operating schedule.
Also compare control options, safety features, and routine maintenance requirements. Clear controls and accessible components can make operation and upkeep more straightforward. Before making a decision, confirm that the machine fits your workspace and production line, and check the availability of installation guidance, technical support, and replacement parts. Finally, evaluate the total cost of ownership, including energy use, maintenance, and operating costs, rather than focusing only on the initial purchase price.
Yichun Electronic